
Robinets
Showing 1969–1970 of 1970 results
-

MF9.0 X 1.00 Ebauch Tarauds A Main Warwick - Metrique Fin
Item #: TA36092
-

MF9.0 X 1.00 Tarauds A Main Warwick - Metrique Fin Jeux
Item #: TA36095
Clarkson-Osborn products are sold strictly through authorized distributors and intended for industrial, wholesale, and volume purchasing.
Become an Authorized DistributorShowing 1969–1970 of 1970 results
Item #: TA36092
Item #: TA36095
When cutting precise internal threads, maximizing tool life, and eliminating the catastrophic cost of a broken tool inside a finished part are your top priorities, Clarkson-Osborn Tools delivers. As Canada’s premier authority on high-precision threading tools, we supply an elite lineup of industrial-grade machine and hand taps. From high-speed, automated production runs in automotive plants to difficult deep-hole threading in aerospace components, our taps deliver exact thread tolerances, clean chip control, and extreme durability.
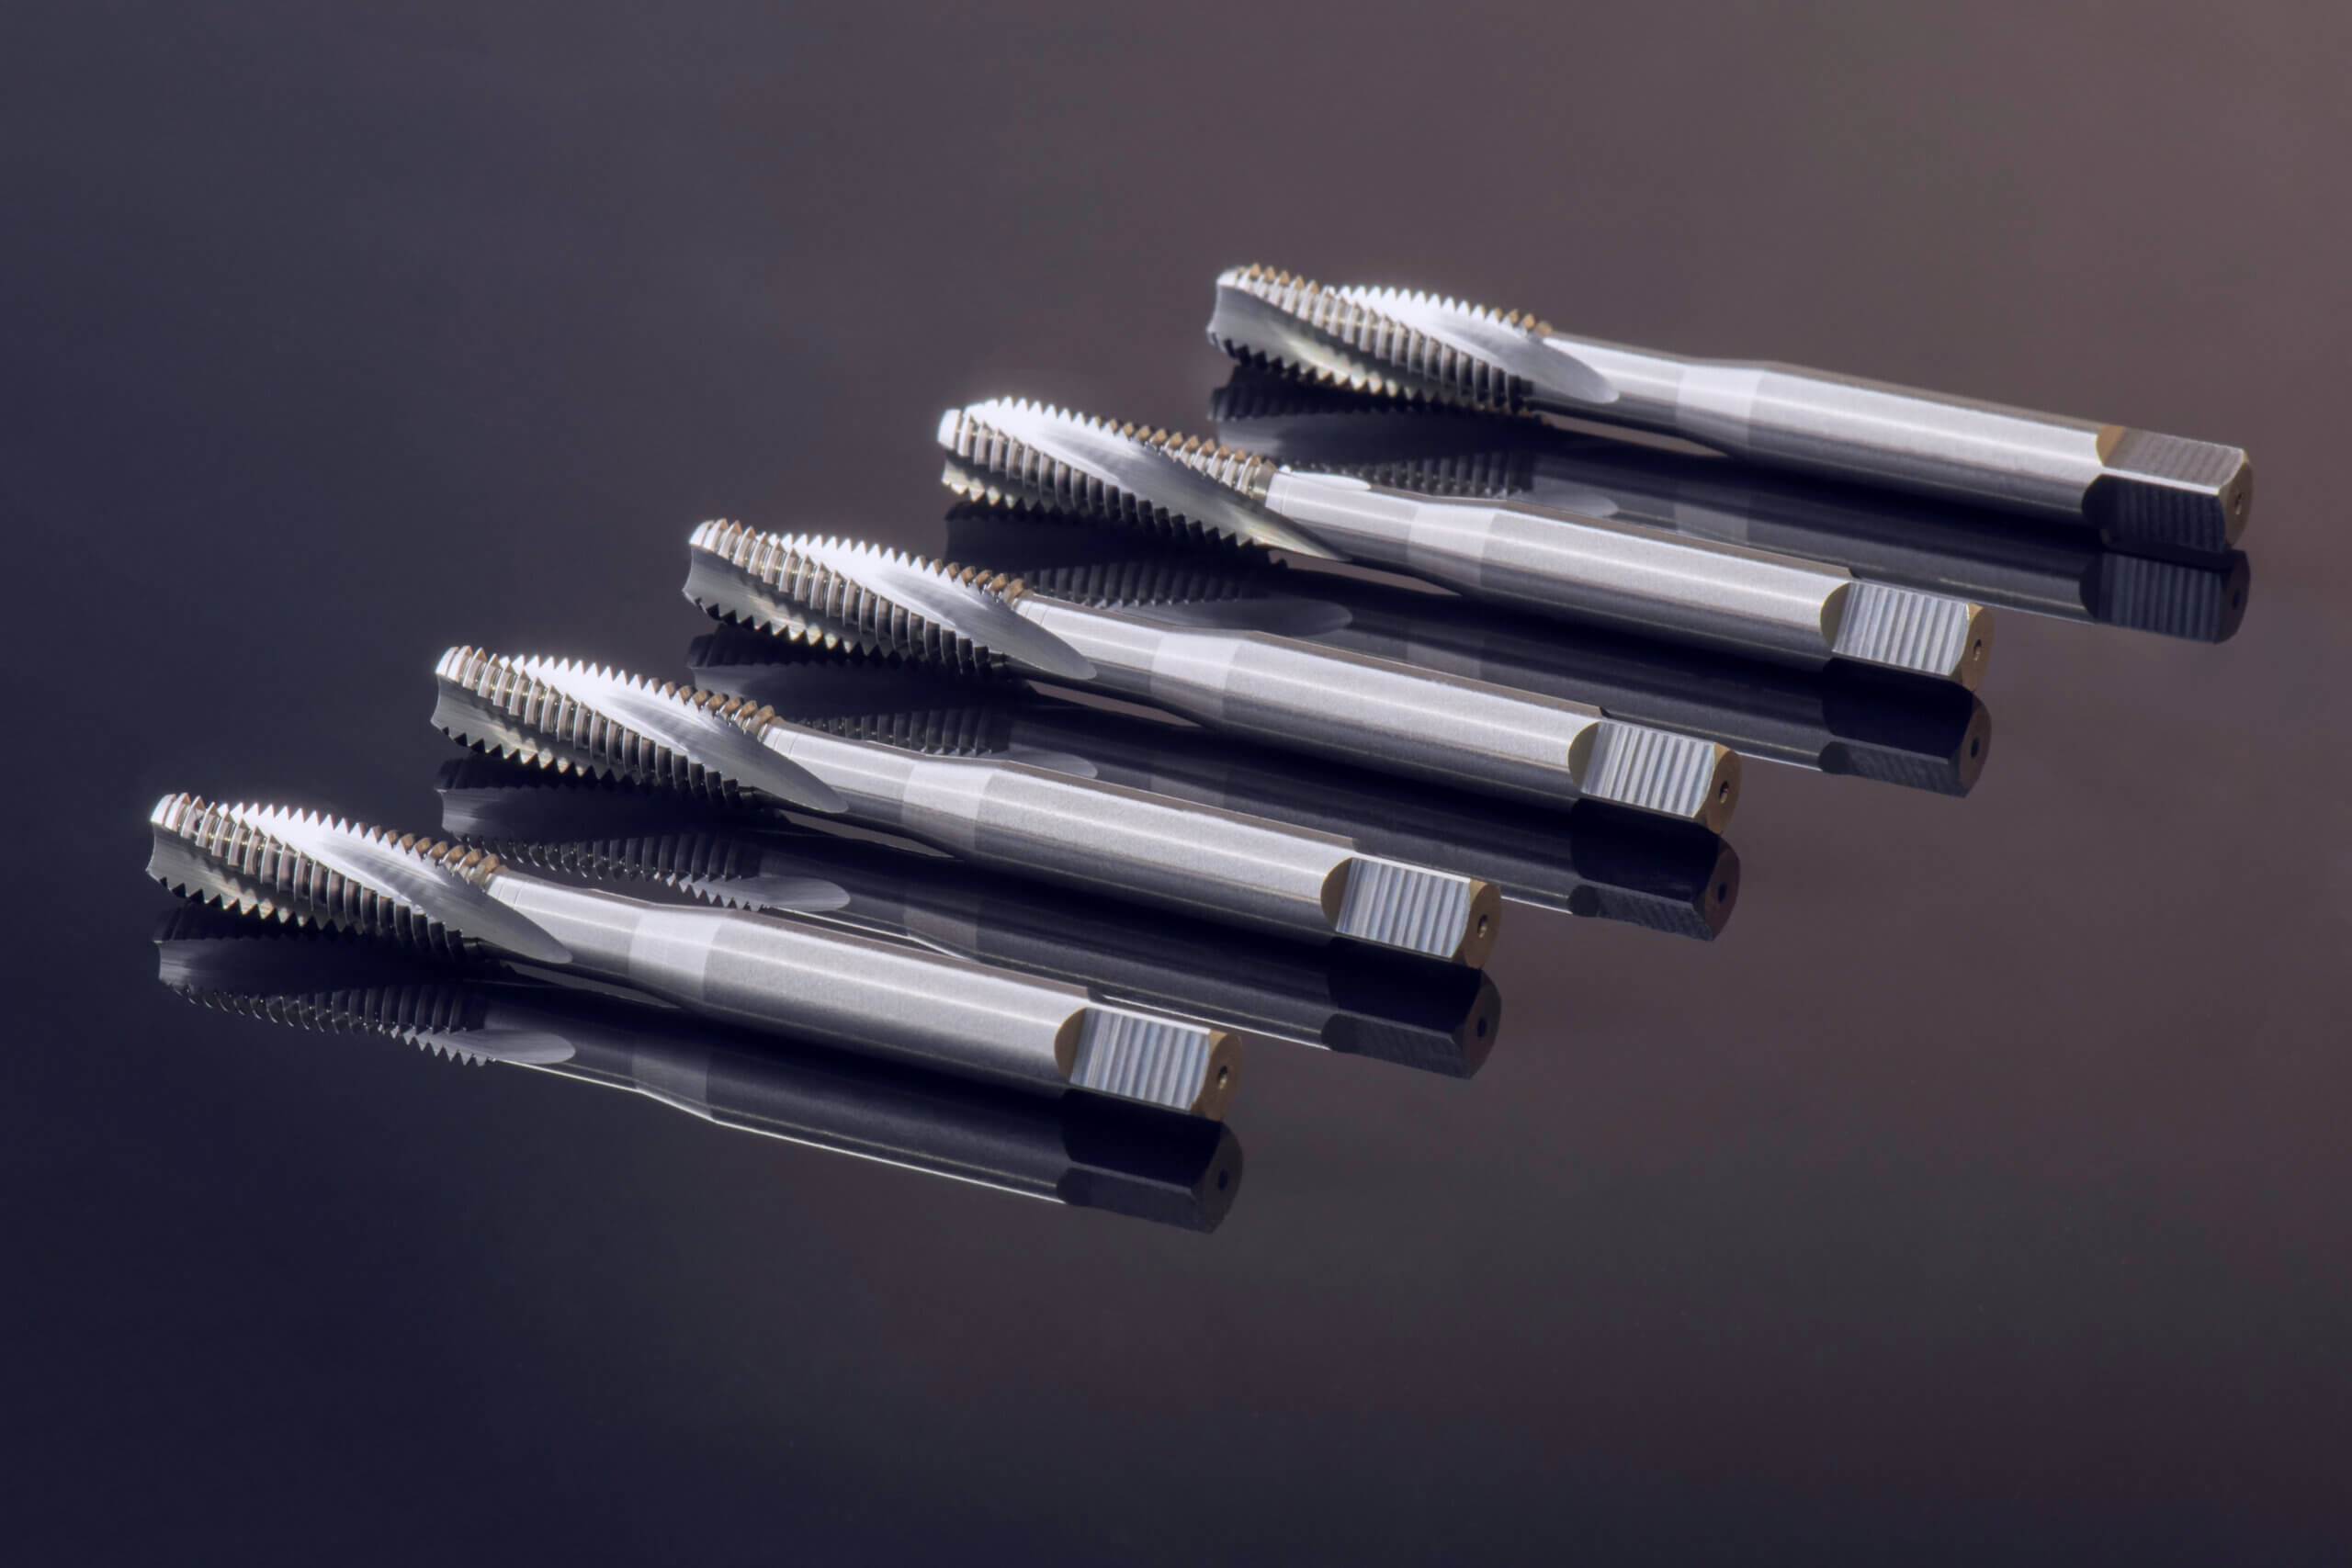
Explore our extensive technical inventory of premium threading taps. Whether your operation requires aggressive spiral point taps for through-holes, specialized spiral flute geometries for lifting chips out of deep blind holes, or rugged hand tap sets for versatile toolroom maintenance, we stock the advanced substrates and surface treatments required to keep your production lines moving efficiently.
Selecting the proper tap configuration requires matching your machine’s rigidity, spindle speed, and workpiece hardness to the correct flute geometry and chamfer length. Utilizing the wrong tap style can result in chip packing, torn thread flanks, or immediate tool breakage. Our catalog features specialized cutting and forming geometries engineered to optimize thread quality across all ferrous and non-ferrous metal groups.
The chamfer refers to the tapered cutting teeth at the front of the tap that distribute the chip load:
To prevent binding, chip welding, and tool failure, match your industrial material group to the correct metallurgical composition and surface coating:
| Tap Substrate / Coating | Best Used For | Key Advantages |
|---|---|---|
| Solid Carbide | Cast iron, abrasive plastics, aluminum, high-volume CNC. | Ultimate hardness, incredible wear resistance, holds strict tolerances over long runs. |
| Cobalt Alloys (M35/M42) | Stainless steels, titanium, high-tensile alloys, structural steel. | Superior red-hardness; cutting edges resist heat breakdown under heavy loads. |
| High-Speed Steel (HSS) | Various steel grades, Carbon steels, aluminum, brass, copper, general maintenance. | Outstanding structural toughness, highly resistant to shock/vibration, economical. |
| TiN / TiAlN Coatings | High-speed production, dry tapping, abrasive metal groups. | Drastically reduces friction, lowers cutting temperatures, expands tool life by 300%. |
For more than 50 years, Outils Clarkson-Osborn has been Canada’s trusted partner for high-precision manufacturing, fabrication, and maintenance engineering. We back our internal threading inventory with elite quality controls:
An H-limit (or D-limit for metric) designates the specific pitch diameter tolerance zone of the tap. Each increment (e.g., H3 vs. H5) represents an increase of 0.0005 inches over the basic pitch diameter. CNC programmers select specific H-limits to ensure that even after applying protective plating or factoring in minor tool wear, the finished internal thread stays perfectly within blueprint specifications (such as a 2B or 3B fit class).
Tap breakage in blind holes is almost always caused by chip compaction. If you use a standard straight flute or spiral point tap in a blind hole, the chips accumulate at the bottom, jam the tool, and cause it to snap under torsional torque. To fix this, switch to a spiral flute tap to pull chips out of the hole, ensure your pilot hole is drilled sufficiently deep, and use a high-quality thread cutting fluid.
No. Thread forming (roll) taps require the workpiece material to be ductile so it can flow and mold into shape. Ductile materials typically have an elongation factor of 5% or greater (such as aluminum, brass, copper, and low-carbon mild steels). Brittle materials like cast iron, or hard materials like tempered tool steels, will not flow; attempting to use a forming tap on them will result in immediate tool destruction.
